Your challenges
Water scarcity, stricter discharge requirements, and rising operating costs are making water reuse and increasingly important part of industrial water management.

Limited freshwater availability
Freshwater supplies are becoming less predictable in many regions. Reducing dependence on freshwater sources can help protect production continuity and support long-term water resilience.

Challenging water quality
Industrial water and wastewater can contain dissolved salts, ions, metals, organic compounds, and other contaminants that require advanced treatment before the water can be reused.

Increasing operating costs
Water abstraction, wastewater discharge, and treatment costs can all affect your operating expenses. Efficient water treatment and higher recovery can reduce the volume of water that needs to be discharged or replaced.

Reliable operation
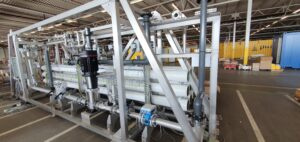
Membrane fouling and changing feedwater conditions can affect performance and availability. A robust membrane solution needs the right pretreatment, membrane selection, and operating concept for the application.
How does it work ?
Key figures
12-90 m³/h
Feed flow
60-80%
Typical recovery range
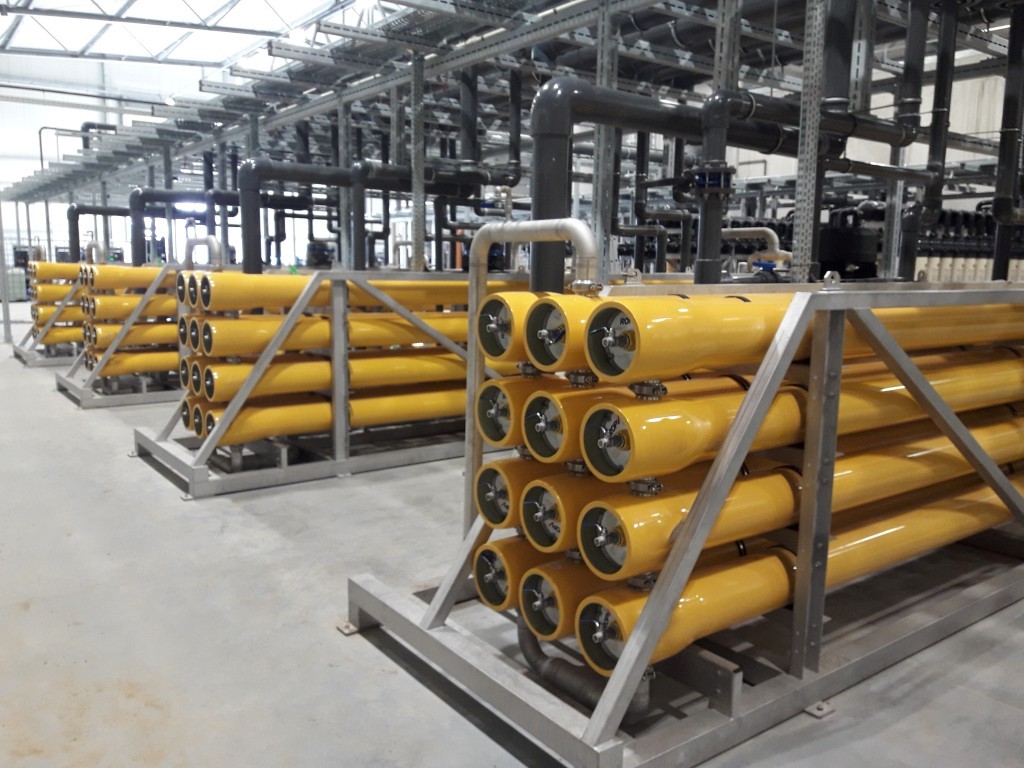
Spiral-wound RO
Membrane type
References
- Industrial
- Pharma & personal care
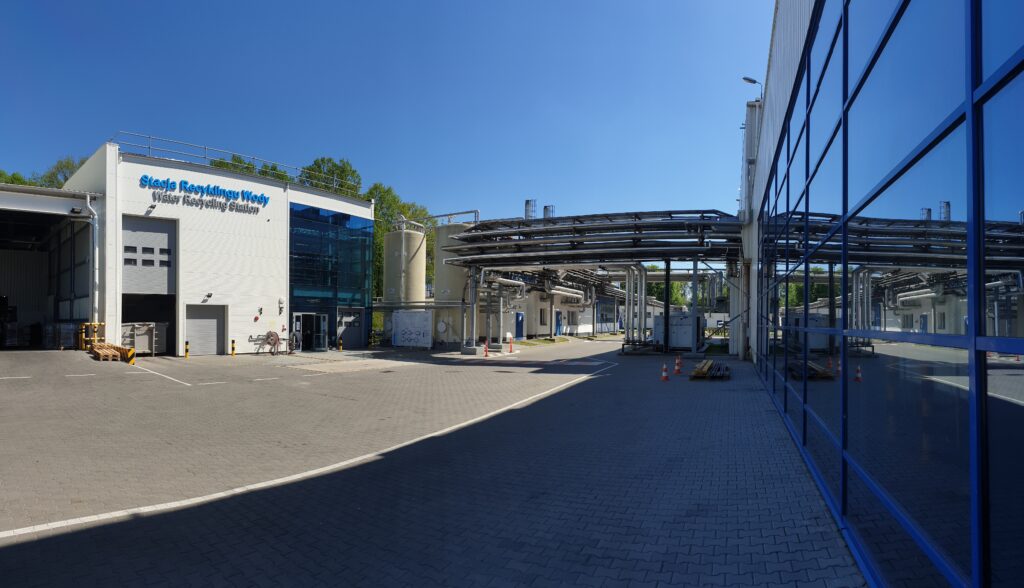
Water reuse for personal care manufacturing to reduce water consumption – L’Oréal
Context
As part of its global sustainability initiative “Sharing Beauty with All”, L’Oréal committed to reducing water consumption, waste output, and CO₂ emissions by 60% compared to 2005 levels. At its Warsaw plant, the challenge was to implement a water recycling system that could recover high-quality water for reuse in production processes, while also showcasing environmental leadership. The project needed to ensure continuous water availability, operational safety, and long-term reliability.
Solution
Nijhuis Saur Industries designed and built a Water Recycling Station using a combination of physical-chemical pretreatment, biological treatment with MBR, ultrafiltration, and reverse osmosis. The system includes the i-DOSE intelligent dosing system for optimized chemical use and online chloride monitoring to manage recovery rates. The plant is fully automated and integrated into the factory’s operations, with a modern design that fits the site’s aesthetics.
- Energy
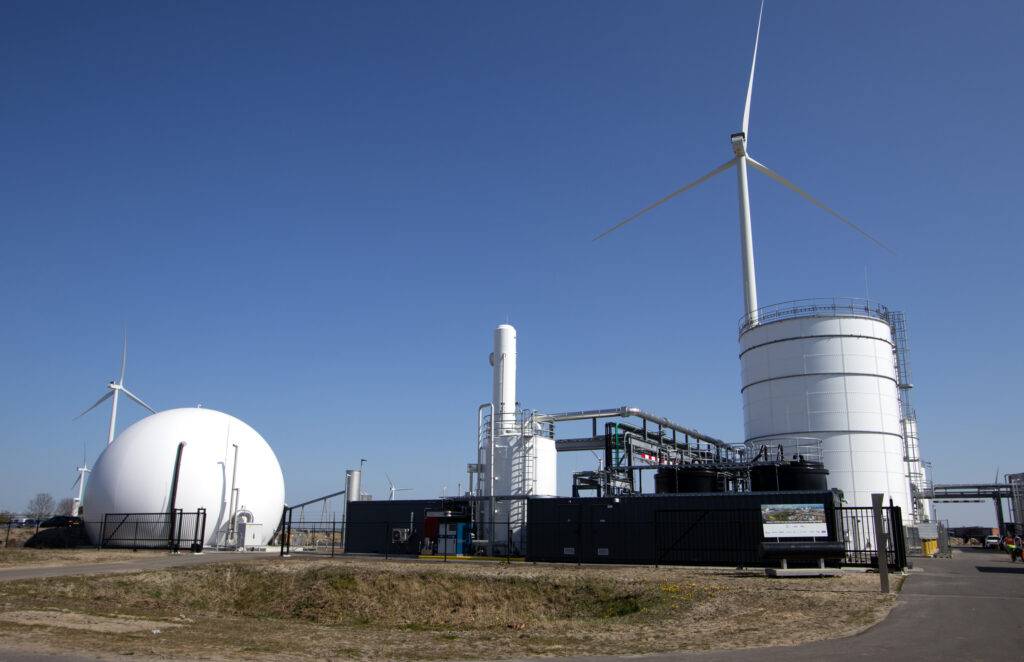
Water reuse and biogas production for industrial operations to reduce dependance on drinking water – DWD Delfzijl
Context
Duurzame Watervoorziening Delfzijl (DWD) is a landmark project in the Netherlands, enabling large-scale industrial transition to alternative water sources. Led by North Water, the initiative provides industrial water from surface water via a treatment facility in Garmerwolde. Nijhuis Saur Industries (NSI) and Econvert Water & Energy contributed significantly with an anaerobic wastewater treatment system and a modular demineralized water (demiwater) installation. The project addresses the growing pressure on drinking water resources and supports sustainable industrial operations in Delfzijl
Solution
NSI and Econvert delivered a comprehensive solution including anaerobic wastewater treatment and a modular demiwater installation. The demiwater system upgrades industrial water to ultrapure quality (<1 µS/cm), suitable for boiler feed and green hydrogen production. The modular setup includes separate containers for UF, RO, membrane degassing, and EDI, allowing off-site construction and rapid deployment. The Econvert-EGSB® treats high-organic wastewater, producing biogas that is desulfurized using Econvert-Dsulph® technology. The biogas is upgraded for use as green gas. The system is designed for scalability and future industrial expansion.
- Industrial
- Food & Beverage
- Waste-To-Energy
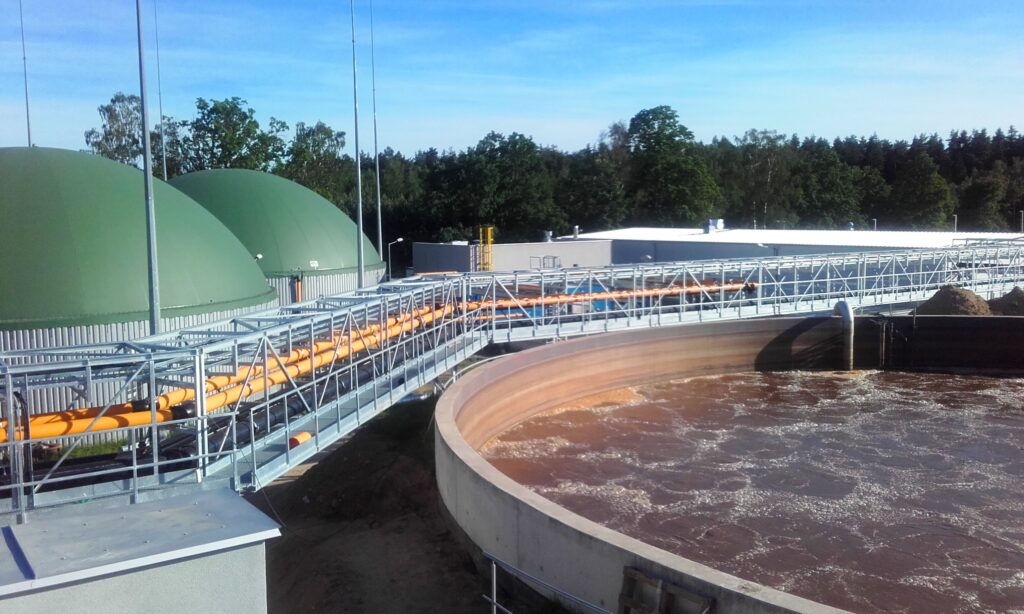
Wastewater treatment and biogas production for poultry processing – Cedrob
Context
Cedrob S.A., a leading and fast-growing poultry producer in Poland, is expanding its slaughtering operations while aiming to minimize environmental impact and secure long-term water availability. Due to site development by extra slaughterlines and rendering facility as well as climate-related pressure on local groundwater resources, additional freshwater abstraction became restricted. At the same time, Cedrob sought to increase production without increasing its environmental footprint.
In partnership with Nijhuis Saur Industries, Cedrob therefore developed an integrated and sustainable water management strategy combining wastewater treatment, water reuse, and waste-to-energy. The objective was to ensure reliable internal water supply, minimize discharge and disposal, and convert organic residues into renewable energy. Today, more than 50 % of the site’s water demand is covered by reclaimed process water.